3 Oftaj Eraroj en Forĝado per Fermita Ŝtabo kaj Kiel Eviti Ilin?
Fermita morta forĝado is commonly used to produce metal parts with reproducible dimensions, superior mechanical qualities, and consistent performance. The method heats a billet inside a die cavity, allowing the material to flow under compressive force until it approaches the desired geometry. Strong components with a good grain structure and relatively low material waste can be produced by forging if the tooling, material, and process parameters are well matched. But the process isn’t simply heating a billet and pressing it into a die. Small decisions concerning material selection, die design, preform development, temperature control, and parameter setup can have a large effect on the end component. In production, these areas might exhibit errors such as incomplete filling, excessive flash, laps, folds, dimensional variation, premature die wear, or cracking. The good news is that many of these problems can be avoided before they become expensive production difficulties. Engineers can reduce risk by analyzing material and tools together, validating the preform and forging parameters, and better controlling heating and cooling. In this article, we highlight three typical errors in closed die forging and offer practical solutions for producers to avoid them.
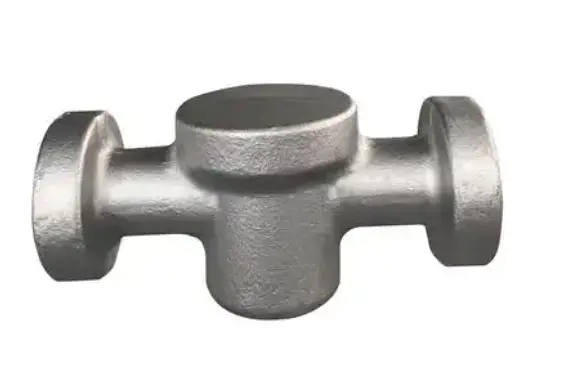
Mistake 1: Choosing the Wrong Material or Treating Die Design as an Afterthought
Match Material Selection to the Part and Forging Process
Material selection is one of the first factors that impacts the outcome of a forging project. If the hot-working qualities of the material are not acceptable for the planned process, then the material may be difficult to forge even if it works well in the finished component.
Engineers need to look beyond the final mechanical requirements. Important concerns are forgeability, required forging temperature, deformation behavior, heat treatment requirements, corrosion or wear resistance, and the intended service environment.
A part subjected to significant mechanical loads might require an alloy with sufficient strength and toughness. However, just choosing an alloy that matches the final strength requirement can present challenges in manufacturing if the material has a small forging temperature range or requires extremely precise process control.
Production also needs to consider the state of the material. The forging procedure can be affected by variations in billet dimensions, surface condition, chemical composition, or incoming material quality. A uniform specification of raw materials and a proper incoming inspection will limit variation between production batches.
One practical way is to look at material selection and production feasibility together. Engineers need to question, “Can this material be successfully forged into this geometry using the equipment and tooling that is available?” Rather than just asking, “Can this material meet the finished-part specification?”
That difference can save costly tooling and process headaches down the road.
Design the Die Around Material Flow.
Even if the material is correct, bad die design might generate major complications. The movement of the heated workpiece during deformation is controlled by the geometry of the die cavity, and a controlled material flow has to be allowed for.
A few of the design features need special mention:
-
Position of the parting line
-
Drafting angles
-
Corner and fillet radius
-
Depth of cavity
-
Geometry of flashland
-
Material volume distribution
-
Areas with large cross-section variations
If the cavity does not flow well, some areas of the material may fill too early while others are underfilled. Too much resistance to the flow of material can also raise the loads in forging and accelerate the die wear.
Another possible concern is sharp corners. They can concentrate distortion and make the material more difficult to flow. Smooth transitions between parts and reduced localized forming issues can be obtained by using appropriate radii.
The separating line should also be selected with the final geometry and flow of material in mind. A separating line placed badly might make die filling difficult, enhance flash, or make cutting harder.
Uzu Simuladon Antaŭ Tranĉado de Produktaj Ŝancoj
Computer-aided design and forging simulation can provide helpful information before costly production tooling is made. Simulation allows engineers to study the material flow, cavity fill, deformation behavior, probable folding zones, and estimated forming loads.
Simulation is no substitute for engineering judgment, but it can assist in finding problems when they are still relatively cheap to fix.
A useful workflow is the following:
-
Define the finished component specifications.
-
Choose an appropriate material for the forging and size of the billet.
-
Develop the geometry of the preform and die.
-
Simulate the flow of the substance and the filling of the cavity.
-
Review possible manufacturability and forming loads.
-
Change tooling or process settings.
-
Once the design is validated, build the manufacturing die.
This method may help lessen the likelihood of finding significant filling or tooling difficulties once production is underway.
Do Not Ignore Dye Maintenance
In production, tooling is subject to repeated mechanical and thermal stress. Over time dies may develop wear, surface damage, distortion, or localized cracking.
Eventually, using worn dies just because they still make parts may cause dimensional difficulties. The right maintenance plan depends on the material of the die, the forging temperature, the production volume, the lubrication conditions, and the geometry of the components.
Frequent inspections should be focused on locations with high contact stress or repetitive material flow. Checking the performance during production runs can also allow manufacturers to set replacement intervals based on actual wear and not just on a preset calendar timetable.
To summarize, the first mistake is not just choosing the wrong material. It deals with material selection, die design, and tooling condition as independent problems. They should be considered as a single manufacturing system.
Mistake 2: Ignoring Preform Design and Using Uncontrolled Forging Parameters
Understand Why the Preform Matters
A fermita die forĝado operation does not always begin with a simple billet entering the final die cavity. For many components, an intermediate preform is required to distribute material before the final forging stage.
The preform has a direct influence on how much material is available in different regions of the die cavity. If too much material is concentrated in one area, excessive flash may develop. If another area receives insufficient material, incomplete filling may occur.
This is especially important for parts with the following:
-
Large differences in section thickness
-
Profundaj kavaĵoj
-
Long projections
-
Multoblaj branĉoj
-
Irregular cross-sections
-
Complex transitions between sections
A properly designed preform moves material closer to where it is needed before the final forming stage. This can reduce the amount of deformation required during the finishing operation and make material flow more predictable.
Control Volume Distribution Before Production
Material volume is fundamental to forging. If the starting volume is insufficient, the die cavity cannot be completely filled regardless of how the press or hammer is adjusted.
On the other hand, excessive starting volume can result in unnecessary flash, higher forming loads, additional trimming work, and greater material consumption.
For this reason, engineers should verify billet and preform volume before production. The calculation should consider the final component volume as well as the material that will enter the flash region and any expected process losses.
Preform dimensions should also be validated against actual equipment capabilities. A theoretically efficient preform may not be practical if it requires a forming operation that the available machine cannot perform consistently.
Do Not Set Forging Temperature and Speed by Habit
Temperature, deformation rate, and forming force all influence how metal flows during forging. However, there is no single parameter combination that works for every alloy or component.
Forging temperature should be selected according to the material and the required deformation behavior. If the workpiece is too cold, deformation resistance may increase and the risk of defects can rise. If it is overheated or held at a high temperature for too long, material properties or surface condition may be affected.
Forging speed also matters. Different equipment and alloys respond differently to deformation rate. A setting that works well for one component may produce different results for another because of differences in geometry, billet size, or heat transfer.
Instead of relying entirely on historical machine settings, manufacturers should establish process windows for each part. These windows can include acceptable ranges for billet temperature, die temperature, forming speed, lubrication conditions, and other relevant parameters.
Use Process Monitoring to Detect Drift
Production conditions can change even when the nominal machine settings remain the same.
For example, repeated forging cycles may alter die temperature. Furnace performance may change. Lubrication may become inconsistent. Tool wear may gradually change material flow. Raw-material variation can also affect the process.
This is why process monitoring is valuable.
Depending on the application, manufacturers may monitor the following:
-
Workpiece temperature
-
Die temperaturo
-
Forming force
-
Press or hammer stroke
-
Ciklotempo
-
Kondiĉoj de lubrikado
-
Dimensiaj mezuroj
-
Equipment alarms or deviations
The purpose is not simply to collect data. The data should help operators identify process drift before it creates a large number of defective parts.
For high-volume production, trend monitoring can be particularly useful. A gradual increase in forming force, for example, may indicate changes in material condition, lubrication, tooling condition, or process temperature.
Inspect for Laps, Folds, and Incomplete Filling
Defect inspection should not be limited to the final dimensions of the component. A forged part may meet certain dimensional requirements while still containing a forming-related defect.
Laps and folds can develop when material flows over itself rather than forming as a continuous surface. Incomplete filling occurs when material fails to reach the required regions of the cavity.
These problems may be associated with unsuitable preform geometry, insufficient material volume, poor die design, inappropriate temperature, or unfavorable deformation conditions.
The most effective response is to identify the source rather than simply increase forming force. Increasing force may not solve a fundamentally poor material-flow pattern and could increase die loading.
Simulation, first-piece inspection, dimensional checks, and process data can be used together to determine where the problem begins.
The second common mistake is therefore relying on machine settings to compensate for poor performance or process planning. A stable forging operation starts with predictable material distribution and a validated process window.
Mistake 3: Using Poor Heating and Cooling Practices
Heat the Workpiece Uniformly
Temperature control is one of the most important variables in fermita die forĝado. The workpiece must reach a suitable forging temperature before it enters the die, but simply reaching a target temperature on the surface is not enough.
A billet can develop a temperature gradient between its surface and core. Complex or large cross-sections can be particularly challenging because heat does not distribute instantly throughout the material.
If different areas of the workpiece have significantly different temperatures, they may deform differently during forging. This can change material flow and increase the possibility of forming inconsistencies.
Manufacturers should therefore consider:
-
Varmiga metodo
-
Furnace or induction equipment
-
Heatinga ritmo
-
Trempa tempo
-
Grandeco de la verko
-
Alojaj karakterizaĵoj
-
Transfer time from heating equipment to die
Gas-fired furnaces and induction systems can both be suitable depending on the component and production requirements. The important point is that the heating process must be controlled rather than based only on visual inspection.
Minimize Temperature Loss During Transfer
The workpiece can begin losing heat as soon as it leaves the heating system. Long transfer distances, delays, unsuitable handling procedures, or extended waiting time before forging can cause significant temperature changes.
This becomes more important when the material has a relatively narrow processing window.
Production planning should therefore consider the complete path from heating to forming. The target is not simply a correct furnace temperature; the workpiece should enter the die within the appropriate process range.
Temperature monitoring equipment, infrared measurement, or other suitable inspection methods can help verify consistency.
Avoid Uncontrolled Cooling After Forging
Cooling is another area where process mistakes can affect the finished component. After forging, the component may retain considerable heat, and its cooling behavior can influence residual stresses, dimensional stability, and the resulting microstructure.
The correct cooling method depends on the material and required properties. Some components may require controlled air cooling, while others may require a specified heat-treatment sequence involving heating, holding, and cooling under controlled conditions.
Rapid or uneven cooling can create thermal gradients within the component. For some materials and geometries, these gradients can contribute to distortion or cracking.
Therefore, post-forging handling should be treated as part of the manufacturing process rather than an afterthought.
Coordinate Forging and Heat Treatment Requirements
Forging and heat treatment should not be planned independently.
The forging operation affects the material's microstructure and deformation history, while subsequent heat treatment is often used to achieve the required mechanical properties and dimensional condition.
Engineers should establish the complete process route, which may include:
-
Raw-material inspection
-
Billet preparation
-
Kontrolita hejtado
-
Prezentanta
-
Fina forĝado
-
Garnizono
-
Kontrolita malvarmigo
-
Varmotraktado kie necese
-
Machining
-
Fina inspektado
This complete view helps prevent a situation where a forging process is optimized for production speed but creates difficulties during later heat treatment or machining.
Use Thermal Simulation for Complex Components
For complicated parts, thermal simulation can provide additional insight into heating, deformation, and cooling behavior.
Simulation can help engineers identify areas that may experience significant temperature differences and evaluate how process changes could affect the component.
For example, a large variation in section thickness in fermita die forĝado may cause some areas to cool faster than others. Understanding this behavior before production allows engineers to consider changes in heating schedules, transfer procedures, die temperature, cooling methods, or post-forging heat treatment.
Simulation should again be viewed as a decision-support tool rather than a substitute for production testing. Physical inspection and process validation remain important.
Build a Feedback Loop Between Inspection and Production
A reliable forging process should improve over time through feedback.
If inspection repeatedly identifies a defect in a specific location, engineers should investigate whether the cause is related to material distribution, die geometry, temperature, lubrication, equipment settings, or handling.
Likewise, if dimensional measurements show a gradual change during a production run, the tooling and process conditions should be reviewed before the deviation becomes widespread.
This feedback loop is particularly valuable for custom components because each part may have different material-flow and tooling requirements.
The third common mistake is treating heating and cooling as routine support operations. In reality, temperature control directly influences deformation behavior, dimensional consistency, and the final condition of the forged component.
A Practical Checklist for More Reliable Closed Die Forging
Before releasing a new forging design to production, manufacturers can use a simple checklist:
materialo
-
Is the alloy suitable for the service environment?
-
Is its forgeability appropriate for the selected process?
-
Are incoming material specifications and inspection requirements defined?
Die dezajno
-
Is the parting line appropriate?
-
Are draft angles and radii suitable?
-
Has material flow been evaluated?
-
Are potential filling problems identified?
-
Is the die material appropriate for the operating conditions?
Antaŭformo
-
Is the billet or preform volume sufficient?
-
Is material distributed according to the final geometry?
-
Has the preform been validated through simulation or trials?
Procezaj parametroj
-
Is the forging temperature controlled?
-
Are forming speed and force appropriate?
-
Are lubrication conditions consistent?
-
Is process data being monitored?
Temperatura kontrolo
-
Is the workpiece heated uniformly?
-
Is transfer time controlled?
-
Is post-forging cooling appropriate for the material?
-
Are heat-treatment requirements incorporated into the overall process plan?
inspektado
-
Are dimensional inspections defined?
-
Are surface defects checked?
-
Are non-destructive testing requirements established when necessary?
-
Are production trends reviewed to identify process drift?
This checklist cannot replace engineering validation, but it provides a practical way to identify common risk areas before they become costly production problems.
konkludo
sukcesa fermita die forĝado depends on much more than applying sufficient force to a heated billet. The quality of the final component is influenced by decisions made throughout the manufacturing chain, from material selection and die design to preform development, process parameters, heating, cooling, and inspection.
The three mistakes discussed in this article are closely connected. Choosing an unsuitable material or poorly planned die can create material-flow problems. An incorrect preform or uncontrolled forging parameters can lead to incomplete filling, excessive flash, or other defects. Poor heating and cooling practices can introduce additional risks related to deformation, residual stress, microstructure, and dimensional stability.
Manufacturers can reduce these risks by validating material and tooling decisions early, using simulation where appropriate, controlling process parameters, monitoring production conditions, and treating thermal management as an integral part of the forging process. A disciplined approach not only helps reduce scrap and rework but also makes production more predictable.
For companies looking for customized forged components, Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides forging, casting, and machining capabilities for industrial applications. Welong states that it has more than 20 years of industry experience and operates under quality-management and industry certification requirements. Its integrated manufacturing capabilities can support projects that require multiple processes, from initial metal forming through subsequent machining and inspection.
For a new closed-die forging project, involving the supplier during the design stage can also be beneficial. Early discussion of material selection, die configuration, preform design, tolerances, machining allowances, and inspection requirements can help identify manufacturing risks before production tooling is committed. To learn more about how Welong can support your manufacturing needs, contact them at info@welongpost.com.
FAQ
1: Kio estas fermita forĝado?
Closed die forging is a metal forming process where heated metal is shaped between two dies containing a pre-cut profile of the desired part, offering improved strength and reduced material waste.
2: Why is material selection important in closed die forging?
Proper material selection is crucial as it affects the final product's properties, such as strength, durability, and resistance to wear and corrosion, ensuring optimal performance for the intended application.
3: How can incomplete filling be prevented in closed die forging?
Incomplete filling can be prevented by optimizing preform design, fine-tuning forging parameters, and implementing advanced process monitoring and control systems.
4: What role does die maintenance play in closed die forging?
Regular die maintenance is essential to prevent wear, deformation, and failure, ensuring consistent quality and productivity in closed die forging operations.
5: How can thermal simulation improve closed die forging processes?
Thermal simulation tools help identify potential hot spots or cold regions, optimize heating and cooling strategies, and predict residual stresses, leading to improved product quality and consistency.
Referencoj
1. Smith, JR, & Johnson, AB (2019). Altnivelaj Teknikoj en Forĝado per Fermita Ŝtablono: Ampleksa Gvidilo. Journal of Manufacturing Engineering, 45(3), 278-295.
2. Brown, TL, & Davis, CM (2020). Strategioj por Materiala Selektado por Optimuma Forĝada Elfaro per Fermita Ŝtabo. Materialscienco kaj Inĝenierarto: A, 780, 139185.
3. Wilson, EK, & Thompson, RS (2018). Proceza Optimigo en Forĝado per Fermita Ŝtablono: Revizio de Lastatempaj Progresoj. Internacia Revuo pri Altnivela Fabrikada Teknologio, 96(5-8), 1853-1872.
4. Lee, SH, & Park, KT (2021). Teknikoj pri Termika Administrado por Plibonigita Kvalito en Forĝado per Fermita Ŝtabo. Journal of Materials Processing Technology, 291, 116989.
5. Garcia, MA, & Rodriguez, FJ (2017). Simulad-Movitaj Dezajnaj Aliroj por Optimigo de Fermit-Forĝada Procezo. Procedia Engineering, 207, 1907-1912.
6. Anderson, PL, & White, DR (2022). Emerĝantaj Teknologioj en Forĝado per Fermita Ŝtablono: Ŝancoj kaj Defioj. Journal of Manufacturing Systems, 62, 216-228.

Share your inquiry, get the quotation accordingly!

Ĉinio WELONG - Via Fidinda Partnero en Metalaj Solvoj

