Atingante Streĉajn Tolerancoj per la Pulvora Metalurgia Procezo
In precision manufacturing, dimensional consistency can be just as important as material strength or production cost. For components with repeatable geometries and high production volumes, pulvor metalurgio can provide a route to near-net-shape fabrication with less material waste and machining requirements. But it’s not just a matter of squeezing metal powder into a die and sintering it to tight tolerances. Powder properties, tooling precision, compaction density, sintering parameters, dimensional shrinkage, and post-processing all affect the end outcome. For the manufacturer and the purchasing engineer, it is important to understand how these variables interact to determine whether powder metallurgy is acceptable for a precise component. This guide outlines the primary factors that determine dimensional accuracy and how manufacturers can design a more robust tolerance-control strategy.
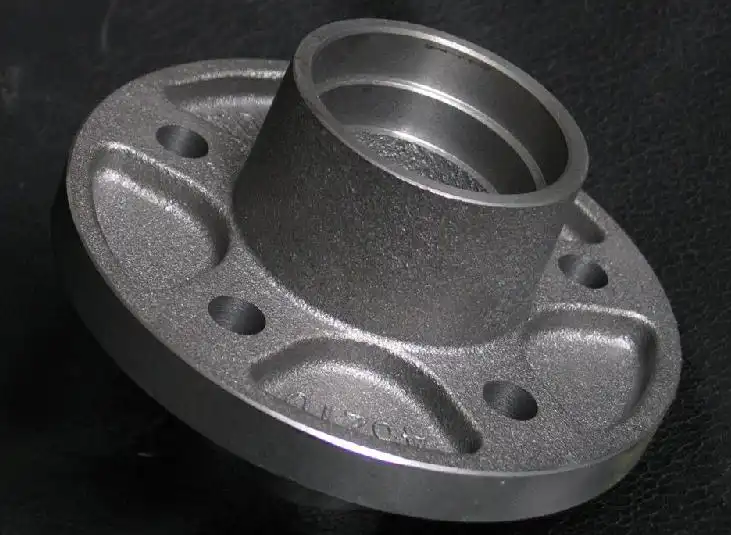
Understanding What Controls Dimensional Accuracy in Powder Metallurgy
The powder metallurgy components are manufactured via a set of interrelated activities. First, the metal powder is selected and manufactured according to the requirements of material and component properties. The powder is then pressed in a die to generate a green part, which is finally sintered so that the particles connect and the part achieves its final metallurgical qualities.
Dimensional alterations may occur at various stages in this sequence. The powder may not be equally distributed throughout the die. Density gradients may arise due to compaction, especially in parts with variable cross-section thicknesses. During the sintering process, the compact generally experiences shrinkage or other dimensional changes as the particles bond and the pore structure changes.
Therefore, the control of the tolerance should be performed during the design of the component and not after the part has been built. The successful execution of a powder metallurgy program calls for careful consideration of the interaction of material selection, tooling, pressing conditions, furnace settings, and inspection needs.
A good way to look at this is to break dimensional control down into five areas:
-
Pulvoraj ecoj
-
Farado de iloj kaj ĵetkuboj
-
Uniformity of Compaction
-
Control of Sintering
-
Sintering sizing or machining after
It is often more beneficial to control these areas simultaneously rather than trying to correct dimensional variance solely at the final inspection step.
How Powder Selection Affects Final Part Tolerances
Controlling Particle Size and Powder Flow
The initial powder properties have a direct impact on filling, compaction, density dispersion, and sintering behavior. Hence, in choosing a powder for a precision component, the particle size distribution, particle shape, apparent density, flowability, compressibility, and chemical composition should be taken into account.
Poor flow characteristics of powders might lead to irregular die filling. This may cause uneven filling and lead to discrepancies in green density, which can be translated into differences in dimensional change during sintering.
The morphology of the particle also matters. Spherical or more rounded particles may display distinct flow and packing behavior from irregular particles. The choosing of the right one depends on the material system and compaction technology.
In addition to the nominal chemistry of the powder, manufacturers should take the powder characteristics and the geometry of the component into account for production parts with tight dimensional constraints.
Managing Lubricants and Powder Blending
Lubricants are typically applied during compaction to reduce friction between the powder and the tooling surfaces and to enable part ejection. However, lubricant content and distribution should be carefully monitored.
Over- or uneven distribution of lubricant might influence the powder packing and the later removal during the first sintering phases. Inadequate control of the blending could also result in changes in composition or density from batch to batch.
Controlling the mixing procedures, selecting proper lubricants, and consistent storage conditions may ensure that the powder behavior is repeatable. Batch traceability is very useful for high-volume production, where you can correlate dimensional data to specific powder lots.
Designing Tooling for Repeatable Dimensions
Building Accuracy Into the Die and Punch Design
Tooling is one of the most critical aspects of dimensional repeatability. The die controls many of the exterior dimensions of the part, whereas punches and cores regulate other aspects such as internal diameters, steps, recesses, and holes.
The tool designer must consider not only the nominal dimensions of the completed part but also the expected dimensional change during sintering. Knowledge in material and processing is required to correlate the compacted green portion with the final sintered part.
Sharp changes in geometry may also cause inhomogeneous filling or density distribution. Where the application allows, appropriate radii, transitions, and wall thicknesses can make compaction more predictable.
For parts with several critical dimensions, the tooling design should identify those that are immediately formable and those that may require sizing or machining after sintering.
Accounting for Tool Wear Over Production Runs
Tooling does not remain dimensionally consistent over a big production run. Repeated compaction cycles can eventually affect die walls, punches, and other wear surfaces.
Even relatively minor changes in tool condition can affect crucial dimensions when a component has stringent tolerance requirements. Regular inspection and preventative maintenance are vital to ensure uniformity between early and later production batches.
Ideally, a dimensional control program would contain tools inspection records as well as part inspection data. This allows manufacturers to assess if dimensional drift is due to powder variation, process conditions, or tooling wear.
Establishing a Stable Temperature Profile
Sintering is an important step, as it is at this stage where the compact develops its metallurgical structure and dimensional changes occur. The last component can be affected by boiler temperature, heating rate, soak time, cooling rate, environment, and loading arrangement.
A steady, reproducible furnace profile will reduce batch-to-batch fluctuation. Multi-zone furnaces can offer more controlled heating settings, and proper environment control can prevent undesirable oxidation or other reactions.
The optimum sintering profile is a function of the powder system. It is not necessarily the same temperature cycle for all pulvor metalurgio systems, such as iron-based materials, stainless steels, copper-based materials, etc.
The sintering cycle of precision parts should be determined according to the material specification and production needs, instead of treating temperature as an isolated parameter.
Managing Sintering Shrinkage
One of the main reasons that the dimensions of powder metallurgy parts cannot be obtained from the final drawing is sintering shrinkage.
The degree of dimensional change varies on green density, the powder composition, particle properties, sintering temperature, atmosphere, and component geometry.
Tooling dimensions may therefore have to be changed depending on historical process data and validation experiments. An experienced maker of similar materials and geometries can build on prior production data to increase the predictability of new tooling.
Dimensional compensation should also be able to discriminate crucial features from non-critical ones. Not all the dimensions require the same control, and the application of unreasonably tight tolerances to all features might raise tooling and manufacturing costs.
Using Process Monitoring to Improve Repeatability
Tracking Key Variables During Production
Modern production systems can collect process data from powder preparation, compaction, and sintering. Monitoring this information can help identify changes before they result in a large quantity of nonconforming parts.
Useful process variables may include:
-
Powder batch information
-
Powder moisture and storage conditions
-
Plenigu pezon
-
Compaction pressure
-
Press cycle parameters
-
Tooling condition
-
Forna temperaturo
-
Fornega atmosfero
-
Sintering cycle time
-
Part dimensions after sintering
The objective is not simply to collect more data. The important point is to identify which variables have a measurable relationship with dimensional performance.
Connecting Process Data With Inspection Results
Dimensional inspection becomes more valuable when the results can be traced back to specific production conditions.
For example, if a critical bore gradually becomes undersized over several production runs, the manufacturer can compare the measurement trend with tooling wear, powder batches, and process settings.
This approach makes troubleshooting more systematic. Instead of correcting dimensions only through final machining, engineers can investigate the source of the variation and determine whether the underlying process should be adjusted.
When Secondary Operations Are Necessary
Using Sizing for Critical Dimensions
Although powder metallurgy can produce near-net-shape components, not every application should rely entirely on the as-sintered condition.
Sizing is one option for improving dimensional consistency. During sizing, the sintered component is placed into a controlled tool and subjected to a defined forming operation that corrects selected dimensions.
This can be particularly useful for components that require more consistent dimensional control than can reasonably be achieved directly through compaction and sintering.
The feasibility of sizing depends on component geometry, material properties, required dimensional correction, and production volume.
Applying Selective Machining Where It Adds Value
For components containing particularly demanding features, selective machining may be more economical and technically appropriate than attempting to achieve every tolerance directly through the pulvor metalurgio procedo.
Ekzemploj povas inkluzivi:
-
Critical bores
-
Precision mounting surfaces
-
fadenoj
-
Specific sealing surfaces
-
Tight positional features
The advantage of a near-net-shape powder metallurgy component is that machining can be limited to the features that actually require it. This can reduce machining time and material removal compared with producing the entire component from solid stock.
The key is to determine the appropriate balance between tooling precision, as-sintered tolerance, sizing, and machining.
Building an Effective Dimensional Inspection Strategy
Defining Critical Dimensions Before Production
Tolerance control becomes much easier when the drawing clearly identifies critical characteristics.
A manufacturer should distinguish between dimensions that directly affect component assembly or function and dimensions that have greater allowable variation.
This helps engineers allocate process-control resources where they matter most. It also prevents unnecessary cost increases caused by specifying extremely narrow tolerances on features that do not require them.
For procurement teams, drawings should clearly identify:
-
Nominalaj dimensioj
-
Dimensiaj toleremoj
-
Geometriaj toleremoj
-
Surfacaj postuloj
-
Materiala grado
-
Varmotraktadaj postuloj, se aplikeblaj
-
Critical functional features
Verifying Dimensions With Appropriate Measurement Equipment
Inspection equipment should be selected according to the geometry and tolerance requirements of the component.
Depending on the part, manufacturers may use calipers, micrometers, gauges, coordinate measuring machines, optical systems, or other dimensional inspection equipment.
Inspection should also consider sampling requirements. For high-volume production, statistical monitoring can help identify gradual process changes rather than relying solely on final inspection of individual batches.
A good inspection system should answer two questions: whether the current parts meet the drawing requirements and whether the manufacturing process remains stable over time.
Practical Design Considerations for Tighter Tolerances
Designing a component specifically for pulvor metalurgio can significantly improve the likelihood of achieving repeatable dimensions.
Engineers should consider whether the geometry is compatible with the pressing direction, whether wall thicknesses are reasonably consistent, and whether critical features can be formed effectively using available tooling.
It is also useful to communicate tolerance requirements early. If a component has a particularly demanding dimension, the manufacturer can determine during the design stage whether that feature should be controlled through direct compaction, sizing, machining, or a combination of methods.
This is often more effective than attempting to force the entire component into an unnecessarily narrow as-sintered tolerance range.
What Buyers Should Provide to a Powder Metallurgy Manufacturer
A detailed technical package can make quotation and process development more efficient.
When requesting a quotation for a precision powder metallurgy component, buyers should ideally provide:
-
A 2D engineering drawing with dimensions and tolerances.
-
A 3D CAD model when the geometry is complex.
-
The required material grade or chemical composition.
-
Annual or batch production volume.
-
Critical dimensions and functional requirements.
-
Postuloj de surfaca finaĵo.
-
Required secondary operations, such as sizing, machining, or heat treatment.
-
Inspection and documentation requirements.
Providing this information allows the manufacturer to evaluate tooling requirements and determine which dimensions can realistically be controlled through the primary powder metallurgy process.
For OEM projects, discussing tolerance requirements before tooling fabrication can also reduce the risk of expensive design changes later in the development cycle.
Why Supplier Experience Matters for Precision Powder Metallurgy?
Achieving tight tolerances is not dependent on one machine or one production parameter. It requires coordination between material selection, tooling, compaction, sintering, inspection, and secondary processing.
For this reason, supplier selection should consider more than the quoted unit price. Buyers should evaluate manufacturing experience, engineering support, quality systems, inspection capability, material knowledge, and the supplier's ability to handle customized components.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. provides customized metal component solutions and has more than 20 years of industry experience. The company operates across manufacturing, casting, machining, and related metal-component services and holds certifications, including API-7-1 and ISO 9001:2015.
For a powder metallurgy project involving demanding dimensional requirements, a useful first step is to provide the supplier with the component drawing, material requirements, production volume, and critical tolerances. The supplier can then assess whether the required dimensions are best achieved through tooling and sintering alone or through a combination of powder metallurgy and secondary operations.
konkludo
Achieving tight tolerances with pulvor metalurgio requires control across the entire manufacturing sequence rather than relying on final inspection alone. Powder characteristics influence filling and compaction, tooling determines the initial geometry, density distribution affects sintering behavior, and furnace conditions influence dimensional stability. When additional accuracy is required, sizing or selective machining can provide further control over critical features.
The most effective approach is to define critical tolerances during the design stage and evaluate how each requirement can be achieved through the available manufacturing route. Careful powder selection, stable tooling, controlled compaction, repeatable sintering, appropriate inspection, and targeted post-processing can work together to produce consistent components at production scale.
For OEMs and purchasing teams, the right manufacturing strategy depends on the component's geometry, material, tolerance requirements, production volume, and cost target. Working with an experienced supplier such as Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd. can help buyers evaluate these factors before production begins and develop a practical route for producing precision metal components with repeatable dimensions.Please mail info@welongpost.com se vi ŝatus instigi datumojn aŭ ekzameni viajn personajn bezonojn kun Welong.
FAQ
1: What are the main advantages of using powder metallurgy for achieving tight tolerances?
Powder metallurgy offers advantages such as near-net-shape capabilities, improved material properties, reduced waste, and the ability to produce complex geometries that are difficult to achieve through conventional machining.
2: How does powder selection impact the ability to achieve tight tolerances in powder metallurgy?
Powder characteristics such as particle size distribution, morphology, and chemical composition significantly influence the final properties and dimensional accuracy of the component. Selecting the right powder is crucial for achieving tight tolerances.
3: What role does tooling design play in achieving tight tolerances in powder metallurgy?
Tooling design is critical for achieving uniform powder distribution and density during compaction. Optimized tooling design helps minimize dimensional variations and ensures consistent results across production runs.
4: How can sintering practices be optimized to improve dimensional accuracy in powder metallurgy?
Implementing precise temperature control, using protective atmospheres, and developing adaptive sintering profiles can help minimize dimensional distortions and improve overall dimensional accuracy during the sintering process.
Referencoj
1. Smith, JA, & Johnson, RB (2019). Altnivelaj Teknikoj en Pulvora Metalurgio por Precizaj Komponantoj. Journal of Materials Processing Technology, 285, 116-128.
2. Zhang, L., & Chen, X. (2020). Optimigo de Sinterigaj Parametroj por Streĉaj Tolerancoj en Pulvora Metalurgio. Pulvora Teknologio, 362, 451-465.
3. Brown, ME, & Davis, KL (2018). Strategioj por prilaborado de iloj por altprecizaj pulvormetalurgiaj partoj. Internacia Revuo pri Pulvormetalurgio, 54(3), 201-215.
4. Lee, SH, & Kim, YJ (2021). Progresoj en Pulvora Selektado kaj Kompaktigo por Minimumigi Sekundarajn Operaciojn en PM. Materiala Scienco kaj Inĝenierarto: A, 812, 141082.
5. Wilson, DR, & Thompson, EA (2017). Optimigo de Procezaj Parametroj por Netformaj Pulvormetalurgiaj Komponantoj. Journal of Materials Engineering and Performance, 26(9), 4312-4325.
6. Garcia, P., & Rodriguez, M. (2022). Atingante Striktajn Tolerancoj en Pulvora Metalurgio: Ampleksa Revizio. Pulvora Metalurgia Progreso, 22(1), 1-20.

Share your inquiry, get the quotation accordingly!

Ĉinio WELONG - Via Fidinda Partnero en Metalaj Solvoj

