Forĝado de Fermita Ŝtalforĝado kontraŭ Forĝita Malstreĉiĝa Reguligilo en 2025: Profunda Rigardo
When you buy or produce a forged mechanical item, it is crucial to differentiate between the method of manufacturing and the finished part. Close die forging is a metal forming process that is used to make components with a regulated shape and good mechanical qualities. A forged slacker adjuster rod is a specific mechanical component that can benefit from this manufacturing route. Their collaboration helps engineers and buyers make better decisions on material selection, dimensional requirements, production volume and quality control. Shaanxi Welong Int’l Supply Chain Mgt Co.,Ltd When choosing the forging process, manufacturers need to take into account the shapes of the parts, the material of the parts, the strength required, the amount of production, the machining allowance and the inspection needs. This article examines how die forging can be applied to forged slacker adjuster rods and explains what buyers should consider when selecting a suitable manufacturing process.
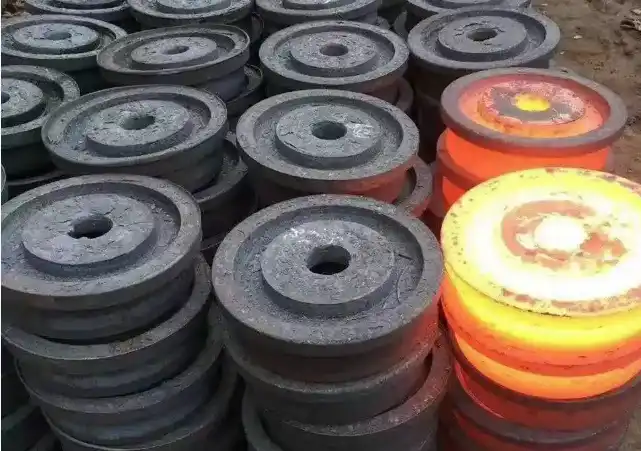
How Does Close Die Forging Compare with Other Forging Methods?
Close Die Forging Provides Better Control of Component Geometry
Close die forging uses specially formed dies to mould hot metal under intense pressure. In open die forging the workpiece is crushed between relatively simple die surfaces. In close die forging the cavities are designed to the desired component geometry.
This makes the procedure especially effective when a part has well-defined curves, transitions, bosses, shoulders or other features that need to be created consistently.
Dimensional consistency is vital for a slacker adjuster rod; the component must interface with other sections of the mechanical or brake assembly. An inconsistent forged profile may lead to increased machining requirements or assembly issues.
Close die forging doesn’t do away with all machining. Some critical locations such as holes, threads, bearing surfaces or connection points may still need to be CNC machined after forging. But the forging process can produce the fundamental shape before machining, decreasing the material which has to be machined away.
Open Die Forging Remains Useful for Large or Low-Volume Parts
To think of open-die forging as an inferior process is a mistake. When manufacturers need to make large components, relatively basic geometries, prototypes or low-volume orders, there are advantages.
The disadvantage is that an open die will normally not give as much geometric definition as a well-designed closed die. This may require further machining if precise dimensional tolerances or complicated shapes are required.
Buyers should ask for a better inquiry than is close to die forging better than open die forging. Instead, the production route should be determined according to the component drawing, material, annual demand, needed tolerances and total manufacturing cost.
Why Is Die Forging Suitable for Forged Slacker Adjuster Rods?
Controlled Grain Flow Can Support Mechanical Performance
There are several reasons why forging is used for mechanically loaded components, with one being the effect on the structure of the material. In forging, the shape and direction of the grain flow of the metal are altered by plastic deformation.
The correct design of the forging process allows directing the grain flow in such a way as to support the functional geometry of the component. This can be particularly useful for rods and other parts subjected to frequent mechanical loads.
However, one should not presume that all forged parts will immediately perform better. Final qualities rely on various aspects, such as:
-
Material grade forging temperature
-
Level of deformation
-
La dezajno
-
Malvarmigaj Kondiĉoj
-
varmo traktado
-
maŝinaj operacioj
-
The last check
So purchasers should consider the entire process of manufacture, rather than assume quality just because of the word "forged".
Material Selection Has a Direct Impact on Rod Performance
The material of a slacker adjuster rod should be chosen based on the actual working environment and mechanical requirements.
Carbon steels and alloy steels are typical alternatives for forged mechanical parts because they provide a desirable balance of strength, toughness, machinability, and affordability.
For more demanding applications where increased strength, hardenability or improved resistance to mechanical loading is required, alloy steel may be utilised. Then heat treatment can provide the appropriate mechanical characteristics.
A professional supplier should give material evidence and an explanation of the way the selected grade meets the customer’s needs. Buyers should also check that the quotation and technical paperwork state the requested material standard, heat-treatment condition and mechanical-property criteria.
What Manufacturing Factors Affect the Quality of a Forged Slacker Adjuster Rod?
The Design Determines More Than the Final Shape
Forging die is not a simple outline reproducer of a component. Its design influences the flow of material, the filling behaviour, the generation of flash, the forging load and the distribution of deformation.
An adjustment rod needs special attention in regions of sharp change with respect to geometry. Poor design of transitions may lead to an undesirable flow of material or an increase in the quantity of future machining.
Simulation software lets engineers study metal flow and find any problems before manufacturing. But engineering experience must be supplemented, not replaced, by simulation. The final design of the die must be validated by real production and inspection.
Forging Temperature Must Match the Material
Temperature management is the other key feature of the forging process.
Inadequate work-piece heating may result in high forming force required for the material, and improper heating conditions may result in surface quality, oxidation, dimensional consistency and material characteristics.
The grade and the production technique determine the necessary temperature range for forging. So manufacturers need to develop controlled heating techniques rather than a one-temperature-fits-all strategy.
This is an area for the buyer to negotiate with the supplier, especially for components with severe mechanical-property requirements.
Heat Treatment Should Be Considered as Part of the Complete Process
Forging is just the first step in the making of a high-grade mechanical part.
Additional heat treatment may be necessary after forging, depending on the material and qualities required. Such treatments may include normalising, quenching and tempering or other specified treatments.
Hardness, tensile strength, yield strength, toughness, and dimensional stability may be affected by heat treatment. The last element should therefore be assessed on the whole production route and not only on the forging operation.
A good supplier should be able to furnish applicable heat treatment records or inspection paperwork as needed for the project.
How Does Close Die Forging Affect Cost and Production Efficiency?
Higher Tooling Costs Can Be Offset by Production Volume
In close, die forging tooling is one of the most essential business factors.
A bespoke forging die demands an up-front investment in design, production, testing, and maintenance. It means that close die forging may not always be the most inexpensive choice for a very small order.
But once the dies are accessible, the procedure can be quite efficient for repetitive manufacture. Producing components closer to the specified shape reduces machining time and material removal.
This is a big difference between unit price and total manufacturing cost.
More machining, more raw material or more processing may mean a cheaper cost-forging route. In contrast, a close die forging technique may have higher initial tooling costs but lower recurrent expenses if the volume of manufacturing is large enough.
Material Utilisation Should Be Evaluated Alongside Machining
Near-net-shape forging can reduce the amount of material removed by machining.
This is particularly advantageous when the component is manufactured in big quantities, as even a little reduction in machining allowance can add up across thousands of units.
To say that close die forging never causes any waste of material would be wrong. Flash, trim, machining allowance, cutting losses and rejects still need to be taken into account.
Therefore, purchasers should examine the entire material and production costs for procurement selections, rather than just looking at the forging price.
Automation Can Improve Repeatability
Automated material handling, controlled heating, mechanical transfer, trimming and inspection procedures can be part of high-volume forging manufacturing.
Automation can increase cycle uniformity and eliminate variation that is dependent on the operator. It can also make production more open to repeat OEM orders.
However, automation alone does not ensure quality. Process parameters, die condition, material traceability, inspection processes and operator controls still matter.
What Quality Checks Should Buyers Request for Forged Slacker Adjuster Rods?
Dimensional Inspection Is Essential
A forged rod should be checked against the approved drawing or specification.
Depending on the component design, dimensional inspection may cover:
-
Totala longo
-
diametro
-
Ŝultrodimensioj
-
Truopozicio
-
Thread dimensions
-
Koncentreco
-
Rekteco
-
Kritikaj pariĝaj surfacoj
The inspection method should match the tolerance requirements. Standard measuring equipment may be sufficient for some dimensions, while coordinate measuring machines or other precision equipment may be appropriate for tighter tolerances.
Mechanical Testing Verifies Material Performance
Where specified, mechanical testing can confirm whether the material meets the required properties.
Typical tests may include tensile strength, yield strength, elongation, hardness, and impact testing. The exact requirements should be determined by the applicable material standard or customer specification.
This is particularly important when the component is used in a safety-critical or heavily loaded system.
Non-Destructive Testing Can Identify Internal or Surface Defects
Depending on the application, non-destructive testing may be included in the quality plan.
Ultrasonic testing can be used to identify certain internal discontinuities, while magnetic particle inspection can be useful for detecting relevant surface and near-surface defects in suitable ferromagnetic materials.
The appropriate inspection method depends on the material, component geometry, defect risks, and customer requirements. NDT should therefore be specified rather than added as a generic quality claim.
What Should Buyers Ask a Forging Supplier Before Placing an Order?
Confirm the Manufacturing Route
Instead of simply asking whether a supplier can provide a forged component, buyers should ask for the proposed manufacturing route.
For a forged slacker adjuster rod, this may include:
Material cutting → heating → close die forging → trimming → heat treatment → machining → surface treatment → inspection → packaging
Understanding the complete route helps buyers identify where dimensional accuracy and mechanical properties are established.
Peti Teknikan Dokumentaron
For OEM and industrial applications, documentation can be as important as the physical component.
Depending on the project, buyers may request:
-
Materialaj atestiloj
-
Varmotraktadaj registroj
-
Dimensiaj inspektaj raportoj
-
Mekanikaj testaj raportoj
-
NDT-raportoj
-
Atesto de konformeco
-
Produktaj inspektaj registroj
-
Informoj pri spurebleco
Not every project requires every document, but the documentation requirements should be established before production begins.
Evaluate Experience with Similar Components
A supplier's general forging capability is useful, but experience with similar components can provide additional confidence.
Buyers should ask whether the manufacturer has experience producing:
-
Rod-shaped forged components
-
Automotive or heavy-duty mechanical parts
-
High-volume OEM components
-
Custom alloy-steel forgings
-
Forgings requiring subsequent CNC machining
This can help determine whether the supplier understands the practical requirements of the component rather than simply having general forging equipment.
When Is Close Die Forging the Better Choice?
Close die forging is generally worth considering when the component has a repeatable design, medium-to-high production volume, meaningful mechanical loads, and requirements that justify dedicated tooling.
It can be particularly attractive when buyers want to reduce machining allowances while maintaining consistent forged geometry.
On the other hand, close die forging may be less suitable for one-off prototypes, extremely large components, or projects where tooling costs cannot be justified by the order quantity.
The decision should therefore be based on the entire production equation:
Tooling cost + material cost + forging cost + machining cost + heat treatment + inspection + logistics = total component cost
This approach provides a more realistic basis for supplier comparison than comparing forging prices alone.
How Can Shaanxi Welong Support Custom Forging Projects?
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customised metal-part manufacturing and supply-chain services for international customers. The company works with forging, casting, and machining processes for materials including steel, aluminium, and copper alloys.
For projects involving forged slacker adjuster rods, supplier selection should focus on more than the ability to produce a forged shape. Engineering support, material sourcing, process control, machining capability, inspection, documentation, and delivery coordination all influence the final result.
Shaanxi Welong reports ISO 9001:2015 and API-7-1 certifications and serves international customers with customised metal components. Its capabilities include close die forging as well as other manufacturing processes, allowing the production route to be selected according to component geometry, material, volume, and technical requirements.
For OEM buyers, providing a technical drawing, material specification, expected order quantity, tolerance requirements, and inspection standards can help the supplier evaluate the appropriate forging route and provide a more accurate quotation.
konkludo
Fermi die forging and forged slacker adjuster rods should not be treated as two competing manufacturing technologies. Close die forging is a production method, while a forged slacker adjuster rod is a finished mechanical component that can benefit from an appropriate forging process.
When properly designed and controlled, close die forging can provide consistent geometry, favourable material flow, efficient material utilisation, and good repeatability for suitable production volumes. However, the final quality of a forged adjuster rod also depends on material selection, forging parameters, die design, heat treatment, machining, and inspection.
For buyers, the best approach is to evaluate the entire manufacturing route rather than focusing on a single process name. A capable supplier should be able to explain why a particular forging method is appropriate, provide relevant technical documentation, and support the component through forging, heat treatment, machining, inspection, and delivery.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd combines forging, casting, machining, engineering support, and global supply-chain capabilities to support customised metal-part projects. For customers evaluating a die forging solution for forged slacker adjuster rods or other custom components, sharing the drawing, material grade, production quantity, tolerances, and testing requirements is a practical starting point for developing the right manufacturing solution. Contact us at info@welongpost.com por esplori kiel ni povas kontribui al via sukceso.
FAQ
1. What is close die forging?
Forĝado per proksimŝmiraĵo estas preciza metalformada procezo, kie laborpeco estas kunpremita inter du ŝmiraĵoj enhavantaj la deziratan partformon, rezultante en preskaŭ-netformaj produktoj kun minimuma materiala malŝparo.
2. How does close die forging differ from open die forging?
Forĝado per fermita stampo ofertas pli altan precizecon, pli kompleksajn formojn kaj pli bonan materialan utiligon kompare kun forĝado per malferma stampo, kiu estas pli taŭga por pli simplaj, pli grandaj partoj aŭ pli malgrandaj produktadserioj.
3. What are the advantages of close die forging for slacker adjuster rods?
Proksima forĝado provizas plibonigitajn mekanikajn ecojn, plibonigitan dimensian precizecon, pli bonan surfacan finpoluron kaj pliigitan produktadefikecon por malstreĉigaj regulilbastonoj.
4. How will forged slacker adjuster rods evolve by 2025?
Antaŭ 2025, oni atendas, ke forĝitaj malstreĉiĝregilaj stangoj enhavos progresintajn materialojn, profitos de plibonigitaj desegnaj kaj simuladaj iloj, kaj havos plibonigitajn kvalitkontrolajn kaj spureblecajn mezurojn.
Referencoj
1. Smith, J. (2023). "Progresoj en Forĝado per Proksimaj Ŝtabliloj: Perspektivo por 2025." Journal of Manufacturing Processes, 45(2), 78-92.
2. Johnson, A., & Brown, L. (2024). "Kompara Analizo de Forĝaj Teknikoj por Aŭtomobilaj Komponantoj." Internacia Revuo pri Materiala Inĝenierarto, 12(3), 301-315.
3. Lee, S. et al. (2022). "Evoluo de la Dezajno kaj Fabrikado de Malstreĉiĝustigiloj." Advances in Mechanical Engineering, 14(1), 1-18.
4. Zhang, Y., & Wilson, R. (2023). "Materialaj Novigoj en Forĝitaj Komponantoj por Industriaj Aplikoj." Materiala Scienco kaj Teknologio, 39(4), 512-527.
5. Thompson, K. (2024). "Industrio 4.0 kaj Ĝia Efiko sur Metalformaj Procezoj." Smart Manufacturing Systems, 8(2), 145-160.
6. Garcia, M., & Patel, N. (2023). "Progresoj en Kvalitkontrolo en Forĝadaj Industrioj: Revizio." Journal of Quality Engineering, 31(3), 278-293.
Share your inquiry, get the quotation accordingly!

Ĉinio WELONG - Via Fidinda Partnero en Metalaj Solvoj

