Kiel elekti inter forĝado per guto kaj forĝado per fermita matrico?
Choosing between Guto Forĝado and closed-die forging requires more than comparing tooling cost or production speed. The two terminologies denote independent characteristics of the forging process but may overlap in actual fabrication. Drop forging is the popular name for the process of shaping metal by repeated strokes of a forging hammer. Closed-die forging is a process in which the hot workpiece is constrained in formed dies in a well-defined chamber. So, depending upon the part and the production needs, a drop forging job can be done with either impression dies or closure dies.
Several interrelated aspects drive the better decision for manufacturers, including part geometry, material, production volume, dimensional requirements, tooling investment, machining allowance, and equipment capabilities. Having these criteria understood helps the selection of a forging path easier, which will produce the desired mechanical properties without extra tooling and manufacturing costs.
How Do Drop Forging and Closed Die Forging Actually Differ?
Forging Method and Die Configuration
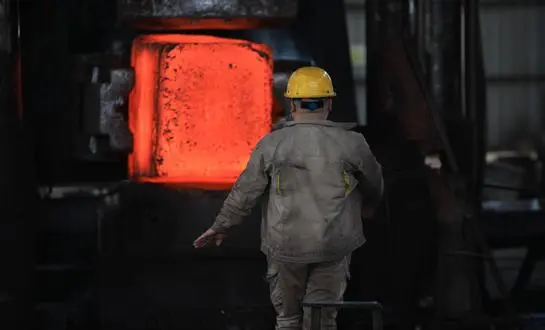
The first step is to distinguish the two notions. Drop forging is the process in which a hot metal billet or preform is formed by the impact of a hammer or similar forging equipment. Depending on the desired geometry, the workpiece can be placed between plain dies or between shaped impression dies. The material can be hammered into the required shape by a succession of blows.
Closed die forging involves the employment of a pair of dies with formed chambers to regulate the flow of material during deformation. The dies close, forcing the hot material into the cavity. Depending on the design, surplus material may be formed as flash around the separating line and then eliminated in a subsequent trimming process.
Therefore, you do not always have to think of drop forging and closed die forging as entirely separate manufacturing categories. A more helpful comparison is how the forging equipment, die arrangement, material flow, and production needs operate together.
This difference is important to a buyer because the choice of a process by name alone may lead to an inappropriate estimate. Normally a provider should analyze the drawing, material specification, part weight, necessary quantity, and tolerances before recommending the final forging path.
Part Geometry and Dimensional Control
Part geometry is one of the most influential aspects in the decision process.
Drop forging is useful for parts whose geometry can be formed by a regulated sequence of hammer blows and for which a moderate machining allowance is acceptable. It can also provide flexibility when a producer has to produce multiple sizes of parts or make design changes during development.
Closed-die forging is particularly beneficial when the part has a known three-dimensional shape that benefits from controlled flow of material in a shaped cavity. Good die design can enhance the repeatability between parts and reduce the amount of material to be eliminated in subsequent machining.
However, one should not assume that forging will yield the final machined dimensions. The needed tolerance should be subdivided into reasonable forging tolerances and machining allowances. Post-forging features such as holes, threads, bearing seats, and precision mating surfaces may still need to be CNC machined.
Grain Flow and Mechanical Performance
One of the main reasons for the usage of forging by manufacturers is the capacity to produce favorable grain flow as opposed to techniques that remove material from a solid block.
Plastic deformation during forging is a function of the workpiece geometry and can result in a directional grain structure, which is beneficial for many load-bearing components. However, the ultimate mechanical performance depends on the whole process and not only on the forging procedure.
The final qualities are affected by material grade, forging temperature, quantity of deformation, cooling conditions, heat treatment, and machining. Therefore, it is better to evaluate a forging process based on the mechanical qualities and material specifications needed rather than assume that one forging process would always create stronger parts.
Manufacturers should additionally consider process qualification, inspection requirements, dimensional inspection, and material traceability for key components.
Which Material Factors Should Guide the Process Selection?
Evaluate Forgeability Before Comparing Processes
Material selection should begin with forgeability. Different metals behave differently under elevated temperature and deformation.
Carbon steels and many alloy steels are commonly forged because their processing windows can be established around suitable forging temperatures. Stainless steels, aluminum alloys, titanium alloys, and other specialty materials may require more carefully controlled heating, deformation, and die conditions.
A material with high deformation resistance can require greater forging force and may place additional demands on the dies and equipment. A material that has a narrower forging temperature range may also require tighter process control.
For this reason, the question should not simply be whether a material can be used with guto forĝado or closed-die forging. The more useful question is which equipment and die configuration can provide stable material flow at the required forging temperature.
Consider Material Utilization and Flash
Material utilization is another important difference in process planning.
In many closed-die forging operations, some excess material is intentionally allowed to form flash. Flash can help promote cavity filling and stabilize the forging process, but it is later removed through trimming. The amount of material consumed therefore depends on the preform design, die design, flash dimensions, and final component geometry.
A well-designed forging process can reduce unnecessary material consumption by optimizing the billet size and preform. This becomes especially important when the raw material is expensive or when the annual production volume is high.
Drop forging may also require additional material depending on the die configuration and machining allowance. Therefore, the best way to compare material efficiency is to examine the complete material balance rather than assuming that one process always produces less waste.
Account for Heat Treatment and Post-Forging Operations
Forging is usually one stage of a larger manufacturing route. Depending on the material and specification, forged parts may require heat treatment such as normalizing, annealing, quenching and tempering, or other specified treatments.
The need for heat treatment should be determined by the material grade and required properties rather than by whether the component was produced by drop forging or closed-die forging.
Machining is another important consideration. Surfaces requiring precise dimensions may need turning, milling, drilling, grinding, or other operations after forging. When comparing two forging routes, manufacturers should calculate the complete production sequence:
raw material → heating → forging → trimming → heat treatment → inspection → machining → final inspection
This broader view provides a more realistic estimate of manufacturing cost than comparing forging costs alone.
How Does Production Volume Affect the Best Forging Choice?
Small and Medium Production Runs
For smaller production runs, tooling investment can have a significant effect on the total part cost.
A simpler forging setup may be attractive when the design is still being developed or when the expected production quantity does not justify extensive tooling investment. Manufacturers producing prototypes, replacement components, or relatively small batches may place more value on tooling flexibility than on achieving the lowest possible unit cost.
This does not mean that closed-die forging is unsuitable for small batches. If the component has a complex geometry or the forging route provides significant advantages in material flow and machining reduction, a more sophisticated die may still be justified.
The key is to compare tooling cost against the expected number of parts rather than choosing a process based solely on production volume.
Alt-Vomena Fabrikado
For high-volume production, repeatability and cycle efficiency become increasingly important.
A properly engineered closed-die forging process can produce large quantities of components with consistent geometry and controlled material flow. Once the tooling has been developed and production is stable, the initial die investment can be distributed across a large number of parts.
Automation can also improve handling, heating, forging, trimming, and inspection operations in high-volume manufacturing environments. This can reduce labor requirements and improve production consistency.
Drop forging can also be suitable for substantial production volumes, particularly when the part geometry and equipment configuration make hammer forging efficient. Therefore, production volume should be treated as one decision factor rather than an automatic rule.
Future Production Growth
Manufacturers should also consider whether today's production quantity is likely to increase.
A component initially produced in a few hundred units may later become a high-volume product. If this possibility is known in advance, it can influence the initial die design and manufacturing strategy.
Tial, a guto forĝado supplier should ideally understand not only the current order quantity but also the expected annual demand, product life cycle, possible design revisions, and target production rate.
What Tooling and Cost Factors Should Be Compared?
Initial Die Investment
Tooling is often one of the first costs considered during forging process selection.
Closed-die tooling can require detailed cavity design, machining, heat treatment, finishing, and inspection. The actual investment depends on part geometry, die material, size, number of impressions, required accuracy, and expected die life.
Gutforĝado tooling can also require engineered dies, particularly when impression dies are used. The difference in tooling cost therefore depends on the actual process rather than the label “drop forging.”
A reliable quotation should separate tooling costs from recurring production costs so the buyer can understand the economic structure of the project.
Life and Maintenance
Die life directly affects long-term manufacturing economics.
Forging dies experience repeated mechanical and thermal loading. Wear can occur around high-contact areas, corners, parting lines, and other features where material flow is concentrated. Die material, heat treatment, forging temperature, lubrication, impact energy, and maintenance practices can all affect service life.
For a long-running production program, the supplier should be able to discuss expected die life and the conditions under which the tooling may require repair or replacement.
Total Cost Per Part
The lowest tooling price does not necessarily produce the lowest total manufacturing cost.
A more useful calculation includes the following:
-
Krudmateriala konsumo
-
Prilabora amortizo
-
Hejta energio
-
Forging cycle time
-
Garnizono
-
varmo traktado
-
Machining
-
inspektado
-
Forĵetu kaj reverku
-
Pakado kaj loĝistiko
For example, a forging route with a higher initial die cost may still be more economical if it significantly reduces machining time and material consumption over a large production quantity.
How Should Buyers Compare Drop Forging and Closed Die Forging?
Match the Process to the Part Drawing
The part drawing should be the starting point for process selection.
Before requesting a quotation, the buyer should provide the supplier with the material grade, finished dimensions, critical tolerances, surface requirements, mechanical properties, heat-treatment requirements, and expected production quantity.
The supplier can then determine whether the guto forĝado geometry is suitable for the proposed die arrangement and identify areas that may require machining allowance or design modification.
Features such as sharp internal corners, deep cavities, thin sections, abrupt changes in cross-section, and difficult-to-fill areas deserve particular attention during design review.
Review Tolerances and Machining Allowance
Not every dimension on a machined component needs to be achieved directly during forging.
A better approach is to identify critical dimensions and determine which surfaces will remain forged and which surfaces will be machined. This allows the forging supplier to design an appropriate allowance without adding unnecessary material.
If the final component requires tight dimensional control, the manufacturing plan should combine forging with suitable machining and inspection rather than expecting the forging stage to provide every final dimension.
Consider Quality Documentation
For industrial procurement, quality documentation is part of the manufacturing decision.
Depending on the application, buyers may request material certificates, dimensional inspection reports, heat-treatment records, chemical composition results, mechanical test results, or other inspection documentation.
A supplier with established quality systems can also provide better traceability from raw material through forging and machining to final delivery.
Which Process Should You Choose?
Choose a drop forging route when flexibility is important.
A drop forging route may be attractive when the component can be efficiently formed through impact forging and the project benefits from flexible tooling or equipment arrangements.
It can be considered for parts where the geometry, material, equipment capacity, and production quantity align well with hammer-based forging. It can also be useful when the manufacturer needs a practical solution for components that do not justify highly complex tooling.
The final decision should still be based on an engineering review rather than the process name alone.
Consider Closed Die Forging When Geometry and Repeatability Are Priorities
Closed die forging is often a strong option when the component has a defined three-dimensional geometry and the production program benefits from controlled die cavities and repeatable material flow.
It becomes particularly attractive when production volume is sufficient to justify tooling investment and when reducing machining allowance or improving dimensional consistency can create meaningful savings.
For complex components, the die design should be reviewed carefully to ensure that the metal can fill the cavity without creating unacceptable defects or excessive forging loads.
Use a Full Manufacturing Cost Comparison
The final decision should be based on the complete manufacturing route.
Instead of asking only “Which forging method is cheaper?" manufacturers should ask:
-
Which process can form the geometry reliably?
-
What equipment capacity is required?
-
How much raw material will each process consume?
-
What tooling investment is required?
-
How many parts are expected over the product life cycle?
-
How much machining will remain after forging?
-
What heat treatment and inspection are required?
-
How easily can production be scaled?
-
What quality documentation is required?
-
Can the supplier support future design or volume changes?
This approach produces a more useful comparison and reduces the risk of selecting a process based on one cost item.
konkludo
Elektante inter Guto Forĝado and closed-die forging require a practical evaluation of the component rather than a simple comparison of two isolated manufacturing methods. "Drop forging" describes an impact-based forging approach, while "closed die forging" describes the way dies contain and shape the heated material, and the two can overlap in an actual production process.
Part geometry, material forgeability, tooling requirements, production volume, dimensional tolerances, material utilization, machining allowance, and equipment capacity should all be considered before making a final decision. For flexible production or suitable simpler geometries, a hammer-based drop forging route may provide an effective solution. For complex shapes requiring controlled cavity filling and repeatability, closed die forging may offer stronger advantages, particularly in larger production programs.
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customized metal components through forging, casting, and machining. With ISO 9001:2015 and API-7-1 certifications, the company supports customers across different industries with manufacturing coordination, quality control, and international supply chain services. For a new forging project, providing the part drawing, material grade, annual quantity, tolerance requirements, and target application gives the engineering team a stronger basis for recommending a suitable manufacturing route.
Retpoŝtu nin ĉe info@welongpost.com se vi bezonas altkvalitajn metalajn partojn aŭ helpon kun via provizoĉeno.
FAQ
1: What is the main difference between drop forging and closed die forging?
Drop forging uses open dies and repeated impacts, while closed die forging uses matched dies that fully enclose the workpiece, offering better dimensional control.
2: Which forging method is better for complex part geometries?
Closed die forging is generally better for complex geometries due to its superior dimensional control and ability to produce near-net-shape parts.
3: Is drop forging or closed die forging more cost-effective for small production runs?
Drop forging is often more cost-effective for small production runs due to lower initial tooling costs and greater flexibility.
4: Which forging method offers better material efficiency?
Closed die forging typically offers better material efficiency due to less waste and the ability to produce near-net-shape parts.
Referencoj
1. Smith, J. (2019). Altnivelaj Forĝaj Teknikoj: Guto kontraŭ Fermita Stampo. Journal of Manufacturing Engineering, 45(2), 78-92.
2. Johnson, A., & Brown, R. (2020). Materialaj Konsideroj en Metalforĝaj Procezoj. Materialscienco kaj Inĝenierarto, 32(4), 215-230.
3. Williams, T. (2018). Kost-efikaj Forĝmetodoj por Malgranda kaj Grandskala Produktado. Internacia Revuo pri Industria Inĝenierarto, 27(3), 145-160.
4. Lee, S., & Park, H. (2021). Kompara Analizo de Gutforĝado kaj Fermitŝilforĝado por Aerospacaj Aplikoj. Aerospaca Fabrikada Teknologio, 18(2), 55-70.
5. Garcia, M. (2017). Progresoj en Forĝado per Fermita Ŝtablono: Precizeco kaj Efikeco. Journal of Materials Processing Technology, 52(1), 112-128.
6. Thompson, R. (2022). Optimigo de Forĝaj Procezoj: Ampleksa Revizio. Progress in Materials Science, 87, 234-250.

Share your inquiry, get the quotation accordingly!

Ĉinio WELONG - Via Fidinda Partnero en Metalaj Solvoj

