Kio estas la optimuma temperaturo por forĝado de aluminio?
Temperature is one of the most important variables in forĝado de aluminio but there is no single temperature that works for every aluminum alloy or every forged component. In actual production, the forging temperature is selected based on the alloy grade, solidus temperature, rate of deformation, size of the billet, die temperature, geometry of the item, and the final qualities required. Hot forging of numerous aluminium alloys is performed over a large range of around 350°C to 500°C (662°F to 932°F), but the useful window becomes much narrower for a specific alloy and technique. Forging references show that many aluminium alloys are forged about 55°C below the corresponding solidus temperature, and published data for aerospace alloys indicate typical forging ranges of about 425–460°C for many 2000-series alloys and 400–440°C for many 7000-series alloys. For instance, 6061 aluminium is often forged at increased temperatures in a range unique to the process, while 7075 is very sensitive to temperature and deformation conditions and requires precise temperature control. The hot forming conditions for 7075 have been reported to be around 350–450°C, appropriate for hot forming. One study found about 420°C as best under its evaluated process parameters. The argument is that the “optimal” temperature should not be taken from a general chart. This should be determined from the alloy specification and then confirmed in the actual forging process.
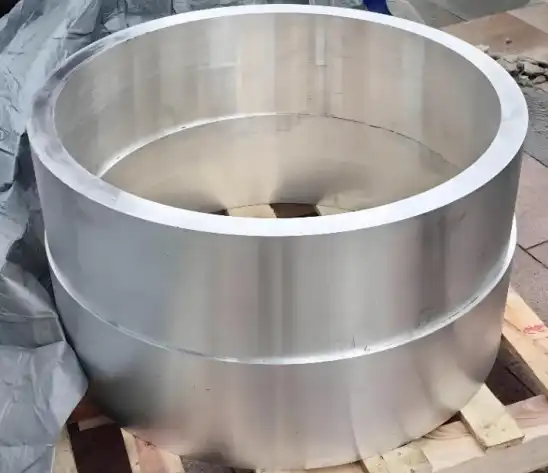
What Determines the Best Forging Temperature for Aluminum Alloys?
Alloy Grade and Solidus Temperature
The first variable to examine is the aluminum alloy. Alloying elements influence the solidus temperature, flow stress, ductility, and deformation response of the material.
For example, 6061 typically has a solidus temperature of about 582°C and a liquidus temperature of about 652°C. This does not indicate that forging of 6061 should take place close to its melting range. A safe manufacturing window must have a sufficient margin below the temperature at which localized melting can occur.
The same approach applies to the 2xxx and 7xxx alloys; however, these alloys have different useful forging windows. References on aerospace materials indicate that many 2000-series alloys are forged at temperatures between 425 and 460 °C, whereas 7000-series alloys are usually forged between 400 and 440 °C.
Consequently, a supplier should verify the precise alloy designation before recommending a forging temperature. “Aluminum” is too vague a material specification for process planning.
Part Geometry and Section Thickness
The actual temperature during deformation is also affected by the shape and size of the forging. A large billet may take longer to heat consistently, while a narrow portion may lose heat quickly after exiting the furnace.
Some complex parts may have deep recesses, thin walls, or large changes in section thickness. These parts may demand tighter control because the workpiece can be at different temperatures in various regions. If one area becomes too chilly, the loads will go up. If another area gets too hot, then the chance of local metallurgical damage is increased.
Therefore, the temperature measured at the furnace or at the surface of the billet does not always represent the temperature of the whole workpiece over the whole forging process.
Deformation Rate and Forging Equipment
The forging machine is important too. Hammer forging, mechanical presses, screw presses, and hydraulic presses can impose highly varied rates of deformation. The Forging Industry Association states that the rate of deformation is a key parameter in the forgeability of aluminum alloys, and some 7xxx alloys are especially sensitive to high rates of deformation.
A quick deformation cycle can also create heat inside the workpiece. During forĝado de aluminio deformation, if the temperature rises sufficiently, the actual temperature of the metal may be higher than the initial temperature of the billet.
Consequently, a temperature that is satisfactory on a slow hydraulic press may not give the same results on a high-speed mechanical press. Process development must take into account both the initial temperature and the temperature change during deformation.
Die Temperature and Contact Conditions
The temperature is another essential issue often disregarded. When a hot aluminum billet comes into contact with a comparatively cold die, heat is rapidly transferred from the workpiece to the tooling.
This can reduce metal flow and make die filling more difficult, particularly in thin and/or intricate areas. In contrast, excessively high die temperature can increase the thermal effects associated with the tooling and, depending on the material, lubricant, and manufacturing cycle, it can shorten the die life.
Also, lubrication is crucial. Unlike many ferrous alloys, aluminum does not develop the same protective scale and can adhere to tooling if the circumstances are not correct. The Forging Industry Association points out the significance of constant lubrication since aluminum alloys might seize, gall, or pressure weld onto steel dies.
What Temperature Range Is Common for Aluminum Forging?
Typical Hot Forging Range
For many commercial aluminum alloys, a realistic hot forging window is somewhere in the range of 350-500 °C, but this should be used as a general reference rather than a universal production specification.
Published references on aluminum alloy forging provide acceptable ranges such as 315–370°C for some 3003 material, 405–460°C for 5083, and 432–482°C for 6061. Other technical sources show hot forging in the region of about 400–500°C as a typical range for aluminum precision forging.
These variances show the need for determining the alloy designation before choosing a process temperature.
So the best question for a purchasing team is not “What temperature do you use for aluminum?” A more appropriate question would be “What temperature window for the billet and die do you recommend for this particular alloy, geometry, forging method, and desired temper?
Example: 6061 Aluminum
6061 is popular because it has a strong combination of strength, corrosion resistance, machinability, and availability. But the forging process needs to be tailored around its special temperature and deformation characteristics.
Published technical information indicates that 6061 forging temperatures are in the general range of 432-482°C. Other reported procedures have utilized temperatures of about 470°C for forged 6061 components.
Do not copy the exact value from another application. Even with the same alloy, different process parameters may be needed for a large structural component, a small precision forging, or a closed-die component.
6061 also has a typical solidus temperature of roughly 582°C; therefore, the forging temperature must be kept low enough to remain well within the melting range while yet giving acceptable plasticity.
Example: 7075 Aluminum
7075 is another essential forging alloy, especially for applications requiring high strength to weight. It is more susceptible to processing conditions than several common aluminum alloys.
7075 was studied, and the forming temperature range was found to be around 350–450°C, with 420°C being the optimal temperature for the deformation conditions studied. Another study proposed a suggested forging range of around 380–440°C for aluminum forging based on ASM for AA7075.
These data indicate that the “optimal temperature” is not a single universal value but is specific to the process.
Why Does Temperature Control Matter During the Entire Forging Cycle?
Heating Must Be Uniform
Reaching the target temperature is only part of the job. The billet also needs to be heated uniformly enough for the material to deform consistently.
If the outer surface is much hotter than the center, the surface may experience excessive deformation while the interior remains relatively resistant to flow. Large billets therefore require appropriate heating time and temperature monitoring.
The heating procedure should be developed around billet dimensions, furnace characteristics, alloy specification, and production cycle rather than using one fixed heating time for every part.
Temperature Can Change During Deformation
The workpiece does not remain at exactly the furnace temperature during forging. Contact with the dies causes heat transfer, while plastic deformation can generate additional heat.
This means that the initial billet temperature and the temperature at the end of the forging stroke can be different. The difference becomes more important for high-speed or high-reduction operations.
For critical components, process development may therefore include temperature measurement at multiple stages rather than relying only on furnace settings.
Final Forging Temperature Also Matters
The final forging temperature can affect the resulting microstructure and the subsequent heat-treatment response.
For heat-treatable aluminum alloys, forging is often followed by solution treatment, quenching, and aging. The Forging Industry Association notes that many forĝado de aluminio alloys are strengthened through subsequent heat treatment, with aging temperatures commonly falling in a much lower range than forging temperatures.
For example, published data for 6061 list a solution-treatment temperature of approximately 529°C and aging temperatures around 160–177°C depending on product condition.
This illustrates an important distinction: forging temperature, solution-treatment temperature, and aging temperature are separate process parameters and should not be treated as interchangeable.
What Happens When the Forging Temperature Is Too Low or Too High?
Risks of Forging Too Cold
When the workpiece temperature is too low for the selected alloy and deformation schedule, flow stress increases. The forging machine must apply more force, and the material may have greater difficulty filling complex die cavities.
Potential problems include the following:
-
incomplete die filling;
-
higher forming loads;
-
increased tool stress;
-
surface defects;
-
cracking in unsuitable alloys or geometries; and
-
additional forging operations.
A lower temperature is therefore not automatically better simply because it may reduce thermal exposure.
Risks of Excessive Temperature
Excessive temperature can be even more serious. Aluminum alloys have relatively narrow processing windows compared with the apparent difference between normal forging temperature and their melting range.
Localized melting or incipient melting can occur before the entire component appears to be molten. Technical forging references warn that temperature increases during deformation can create a risk of incipient melting when the process approaches the solidus temperature.
Overheating can compromise the forging and may lead to rejection rather than simply producing a softer part. This is one reason experienced manufacturers control furnace temperature, billet temperature, die temperature, deformation rate, and process timing together.
How Manufacturers Can Establish an Optimal Temperature Window?
Start With the Material Specification
The first step is to identify the exact alloy and temper requirement. A drawing that simply states “aluminum” is not enough for accurate process planning.
The supplier should confirm the alloy designation, applicable material standard, required temper, mechanical-property requirements, and any customer-specific specifications.
The Aluminum Association's standards provide detailed information on aluminum alloy compositions, tempers, mechanical properties, and product forms, making alloy identification an important foundation for engineering decisions.
Evaluate the Complete Forging Route
The temperature should then be evaluated together with the following:
-
billet dimensions;
-
forging reduction;
-
die design;
-
die temperature;
-
lubrikado;
-
press or hammer type;
-
deformation rate;
-
number of forging stages;
-
transfer time between operations; and
-
post-forging heat treatment.
A temperature that performs well in a laboratory test may not be appropriate for high-volume production if the actual transfer time, tooling temperature, or deformation rate is different.
Verify the Process With Production Data
For demanding applications, temperature selection should be supported by production trials and inspection data.
Useful process records may include billet heating temperature, die temperature, forging start temperature, final forging temperature, heating time, transfer time, and heat-treatment parameters.
The resulting forgings can then be evaluated through dimensional inspection, visual inspection, mechanical testing, metallographic examination, and other customer-specified quality controls.
This approach is more reliable than selecting a temperature solely from a general online table.
How the Right Temperature Improves Aluminum Forging Performance?
Better Die Filling and Formability
A suitable temperature lowers the flow stress enough to allow the aluminum alloy to fill the die without requiring unnecessary forming force.
This is particularly valuable for closed-die components with ribs, bosses, thin sections, and other complex features. Better material flow can reduce the risk of incomplete filling and reduce the need for excessive machining allowances.
More Consistent Mechanical Properties
Temperature control contributes to consistent microstructure and helps the manufacturer maintain a repeatable thermal history.
However, temperature alone does not determine mechanical performance. Alloy composition, forging deformation, cooling, solution treatment, quenching, and aging all contribute to the final result. FIA guidance similarly identifies alloy composition, forging process variables, and final heat treatment as factors affecting the strength of aluminum forgings.
More Stable Production Costs
A well-defined temperature window can also improve production efficiency. Stable process conditions can reduce scrap, unnecessary reheating, die-filling problems, and unexpected tooling issues.
For OEM buyers, this matters because process stability affects more than individual part quality. It can influence production capacity, delivery consistency, inspection costs, and the overall cost of ownership.
What Should Buyers Ask an Aluminum Forging Supplier?
A capable supplier should be able to explain how the forging temperature was selected rather than simply providing a generic temperature number.
Before placing an order, buyers can ask the following:
-
What aluminum alloy and temper will be used?
-
What is the recommended billet forging temperature range?
-
How is billet temperature measured?
-
How is die temperature controlled?
-
What forging equipment and deformation rate are used?
-
How is overheating or incipient melting prevented?
-
What lubrication system is used?
-
What heat treatment follows forging?
-
Which dimensional and mechanical inspections are performed?
-
Can the supplier provide material certificates, inspection records, and relevant process documentation?
These questions help distinguish a supplier with an established forging process from one that simply outsources production and resells finished components.
konkludo
The optimal temperature for forĝado de aluminio is not a single universal number. For many aluminum alloys, hot forging is performed within a broad range of roughly 350–500°C, while the actual production window depends on the alloy, solidus temperature, component geometry, deformation rate, die temperature, and required final properties. Specific alloy examples can vary considerably: published references report approximately 425–460°C for many 2000-series aerospace alloys and about 400–440°C for many 7000-series alloys, while 6061 processes may use a higher window depending on the forging route.
The most reliable approach is to select the temperature from the material specification, validate it through process trials, and control the complete thermal cycle from billet heating through forging and subsequent heat treatment. Avoiding both insufficient temperature and overheating is essential for maintaining formability, dimensional consistency, tooling performance, and final mechanical properties.
For OEM and industrial buyers, the best supplier is not necessarily the one quoting the highest or lowest forging temperature. It is the supplier that can demonstrate why a particular temperature window is appropriate for the alloy, component, equipment, and required performance.
Partner with Welong for Customized Aluminum Forging Solutions
Shaanxi Welong Int'l Supply Chain Mgt Co., Ltd., established in 2001, provides customized metal components for industrial customers and supports forging, casting, and machining requirements. The company states that it holds ISO 9001:2015 and API-7-1 certifications and serves customers in multiple international markets.
Por forĝado de aluminio project, process selection should begin with the actual engineering requirements rather than a generic temperature value. Welong can work with customers to evaluate material grade, component geometry, manufacturing route, machining requirements, quality expectations, and delivery requirements before production. When requesting a quotation, buyers can provide the aluminum alloy designation, component drawing, or 3D model; required temper; quantity; applicable standards; inspection requirements; and target application. These details allow the manufacturing route and forging conditions to be assessed more accurately and help reduce unnecessary process changes later in the project. For more information, contact us at metal@welongpost.com.
FAQ
1: What is the typical temperature range for hot aluminum forging?
Hot aluminum forging typically occurs at temperatures above the material's recrystallization point, usually between 350°C and 500°C (660°F to 930°F), depending on the specific alloy.
2: How does the forging temperature affect the grain structure of aluminum?
Higher forging temperatures generally result in larger grain sizes, while lower temperatures tend to produce finer grain structures, which can impact the material's strength and ductility.
3: Can aluminum be forged at room temperature?
Yes, aluminum can be cold forged at room temperature, but this process typically requires higher forging forces and is limited to less complex shapes and smaller parts.
4: How does the cooling rate after forging affect aluminum properties?
The cooling rate after forging can significantly impact the final properties of aluminum, with faster cooling rates generally resulting in higher strength but potentially lower ductility.
Referencoj
1. Smith, JR, & Johnson, AB (2018). Progresoj en Aluminiaj Forĝaj Teknologioj. Journal of Materials Processing Technology, 256, 112-125.
2. Brown, ET, & Davis, CM (2019). Optimigo de Forĝaj Parametroj por Aluminiaj Alojoj. Internacia Revuo pri Metalgisado, 13(2), 345-358.
3. Wilson, RL, & Thompson, KS (2017). Efiko de temperaturo sur la evoluo de mikrostrukturoj en forĝitaj aluminiaj komponantoj. Materialscienco kaj inĝenierarto: A, 702, 259-271.
4. Anderson, PQ, & Miller, ST (2020). Kompara Studo de Malvarma, Varma, kaj Varma Forĝado por Aluminiaj Alojoj. Journal of Manufacturing Processes, 52, 280-295.
5. Lee, HW, & Garcia, MR (2018). Plibonigo de Ilovivdaŭro en Aluminia Forĝado per Temperatura Optimigo. Wear, 412-413, 89-98.
6. Taylor, FK, & Roberts, GL (2019). Influo de Forĝa Temperaturo sur Mekanikaj Ecoj de Aluminiaj Alojoj. Materialoj & Dezajno, 168, 107638.
Share your inquiry, get the quotation accordingly!

Ĉinio WELONG - Via Fidinda Partnero en Metalaj Solvoj

